A color mismatch between two edge banding orders can turn a regular sale into a costly problem. I may lose customer trust, face returns, and struggle to match furniture panels.
I manage color consistency by keeping approved samples, using clear color specifications, checking new production batches, and working closely with my manufacturer. I also record color data and compare repeat orders against the same reference before accepting new shipments.
In my experience, color consistency is not only a production issue. It also depends on how I place orders, store samples, inspect products, and share information with my supplier. A color name alone may not be enough to guarantee a close match. I need a clear process that both sides can follow every time I reorder the same product.
Why Does Color Consistency Matter Across Repeat Edge Banding Orders?
I know that a product can look correct in one shipment but different in the next. When my customers use both batches on the same furniture project, the color difference may become easy to see. This can lead to complaints and extra costs.
I maintain color consistency by using an approved reference, keeping clear records, and checking each new batch against the original standard. This helps me reduce avoidable differences and protect my customers’ confidence in my products.
How Does Color Consistency Affect Furniture Quality?
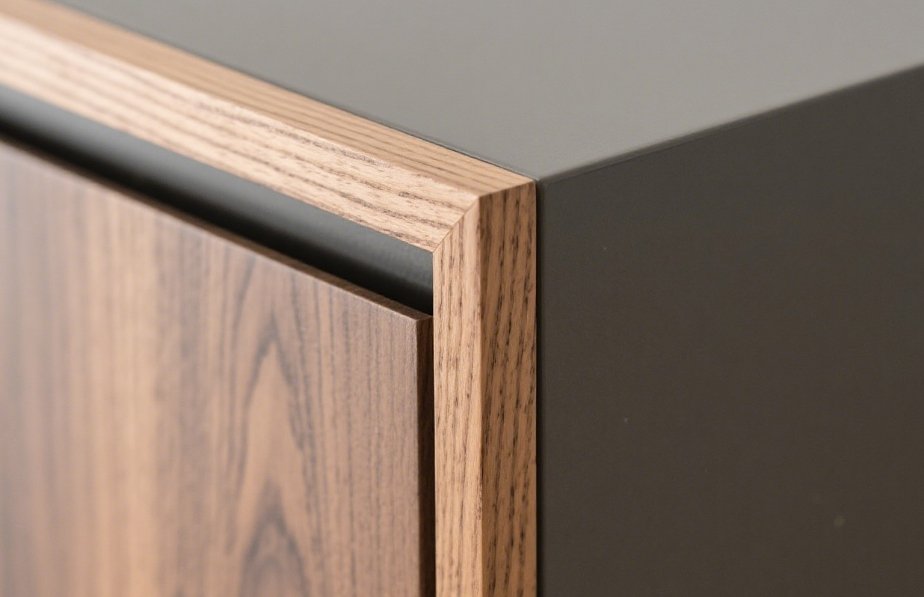
I treat color matching as an important part of the finished furniture appearance. Furniture manufacturers often use edge banding to cover the exposed edges of decorative panels. The edge banding should match the panel as closely as the agreed specification requires.
If the edge banding looks different from the panel, the finished product may appear inconsistent. This matters when customers use the same color across cabinet doors, shelves, desks, or multiple furniture units. Even when the edge banding meets its basic dimensions, a visible color difference may still cause a customer to reject it.
I also consider repeat orders. A furniture factory may purchase the same color several times over a few months. If each order looks different, the customer may find it difficult to maintain a consistent appearance across different production runs.
Why Should I Keep the Same Color Reference?
I do not rely on color names alone. Names such as white oak, warm gray, or walnut can describe many different shades. Different manufacturers may also use different internal color codes for similar colors.
I keep an approved physical sample and a written color reference for each important product. I record the supplier’s product code, panel reference, finish, and approval date. This gives both sides a clear starting point when I place another order.
The International Commission on Illumination (CIE) explains that color can be described using defined colorimetric systems. Its ISO/CIE 11664-4:2019 standard defines the CIE 1976 Lab* color space, which represents lightness and two color dimensions. This gives me a more structured way to discuss color than using names alone.
I still use physical samples because customers need to see how the edge banding looks with the actual panel. Color data supports the comparison, but I do not assume that a single number can replace visual approval under suitable conditions.
What Causes Color Differences Between Edge Banding Production Batches?
I do not assume that every color difference comes from poor production control. The cause may involve raw materials, color formulation, processing conditions, surface finish, or the way people inspect the products.
I investigate these factors before deciding how to correct a problem. I also ask the manufacturer to compare the new batch with the approved reference and review its production records.
How Can Raw Materials and Production Affect Color?
I understand that color consistency depends on more than the color formula. A manufacturer may use different raw material batches or make adjustments during production. These changes can affect the final appearance if the process is not controlled well.
For PVC edge banding, I ask the manufacturer how it manages color formulations, raw material changes, and production settings. I also ask whether the supplier keeps records for each batch. These records can help identify whether a difference began with the materials or during processing.
I pay attention to surface finish as well. Two products may use a similar color formula but look different if their textures, gloss levels, or surface treatments are not the same. I therefore compare products with the same finish whenever possible.
I also check whether the products came from different production runs. A new batch should be compared with the approved standard rather than judged only by its color name or label.
How Can Lighting and Viewing Conditions Affect Color Judgments?
I know that the same sample can look different under different lighting conditions. A product viewed under warehouse lighting may not look exactly the same near a window or under the lights used in a furniture showroom.
The CIE colorimetry framework uses defined viewing and measurement conditions to support consistent color evaluation. I apply this idea by comparing samples under the same lighting conditions and placing them next to each other.
I also avoid comparing one sample under bright daylight and another under warm indoor lighting. I check that both samples have similar surface conditions and viewing angles before making a decision.
| Possible cause | What I may notice | What I should check |
|---|---|---|
| Raw material variation | A batch looks lighter, darker, or less saturated | Material and batch records |
| Color formulation changes | A repeat order does not match the approved sample | Color formula and adjustment records |
| Production variation | Differences between rolls from different runs | Process settings and inspection results |
| Surface finish differences | Similar colors look different in appearance | Texture, gloss, and surface treatment |
| Lighting conditions | The color difference changes with the viewing environment | Lighting and comparison conditions |
| Different reference samples | The supplier and distributor approve different shades | Approved sample and color code |
I do not accept a vague explanation such as “the color is close enough” without checking the agreed requirements. I first identify the source of the difference. Then I decide whether the batch meets the acceptance criteria or needs corrective action.
How Can Distributors Set Clear Color Standards Before Placing Repeat Orders?
I reduce confusion by defining the color standard before I place an order. If I leave color approval to a short product name or an informal message, I may give the manufacturer too much room to interpret the requirement differently.
I use an approved sample, a confirmed product code, and written acceptance criteria. For important products, I also ask the manufacturer to record color measurement results when suitable equipment and methods are available.
What Information Should I Include in a Color Standard?
I start with the physical sample that my customer has approved. I make sure the sample represents the required color and finish. If the edge banding must match a particular decorative panel, I keep the panel reference or a suitable sample of that panel as well.
I then record the product information. This includes the supplier’s color code, material type, thickness, width, surface finish, and any other details that could affect the appearance. I also record the approval date and identify which sample is the current reference.
For repeat orders, I tell the manufacturer to use the approved reference instead of selecting a similar color from its existing range. This is especially important when several colors have similar names.
Should I Use Instrumental Color Measurement?
For products where color consistency is important, I may ask the manufacturer to use a spectrophotometer or another suitable color measurement instrument. The manufacturer can record color values and compare them with the approved reference.
The ISO/CIE 11664-4:2019 standard describes how to calculate coordinates in the CIE 1976 Lab* color space. The ISO/CIE 11664-6:2022 standard specifies the CIEDE2000 formula for calculating color differences from CIELAB values.
These methods can support a more consistent comparison between samples. However, I do not set a universal acceptable color difference without considering the product, surface, customer needs, and measurement conditions. My manufacturer and I should agree on the applicable tolerance before production.
| Color control item | What I record | Why it matters |
|---|---|---|
| Approved physical sample | Reference sample and approval date | Gives both sides the same visual reference |
| Product identification | Color code and material specifications | Prevents confusion between similar products |
| Panel reference | Panel brand, code, or sample where available | Helps confirm the intended match |
| Measurement method | Instrument and agreed test conditions | Makes results easier to compare |
| Color tolerance | Written acceptance limit | Defines an acceptable result |
| Sample management | Storage location and replacement rules | Keeps the reference reliable over time |
I also control changes to the standard. If a customer approves a new color, I update the records and make sure the manufacturer knows which reference is current. I do not allow an old sample and a new sample to remain in use without clear labels.
A written standard does not remove every color difference, but it makes the requirement clearer. It also gives me a stronger basis for discussing quality issues with the manufacturer.
How Can Distributors Verify Color Consistency Before Accepting New Shipments?
I do not wait for my customer to find a color problem after the products arrive. I check the new batch against the approved reference before I release the goods for distribution.
I use visual comparison, product identification, and instrumental measurements when needed. I also keep inspection records so that I can trace the results back to the relevant shipment and production batch.
How Should I Compare a New Batch With the Approved Sample?
I first confirm that the new shipment has the correct product code, material, dimensions, and surface finish. I then take samples from the shipment and compare them with the approved reference under consistent lighting conditions.
I place the samples next to each other and check whether the color difference is visible. I also check more than one roll when the order includes multiple rolls or batches. This helps me identify variation that a single sample may not reveal.
When the customer requires tighter control, I ask the manufacturer to provide color measurement results. I confirm that the results use the agreed method and reference conditions. I do not compare numbers from different methods as if they were automatically equivalent.
What Should I Do When the Color Does Not Match?
I separate the affected products from accepted stock while I investigate the issue. I record the order number, batch number, inspection date, and the samples that show the difference. I also take photos, although I understand that photos alone cannot provide a reliable measurement of color.
I contact the manufacturer and request a review of the batch records. If the results fall outside the agreed tolerance, I follow the corrective action or replacement process that both sides accepted before the order.
| Inspection step | Action | Record |
|---|---|---|
| 1. Verify the shipment | Check product codes and batch labels | Delivery and batch details |
| 2. Select samples | Take representative samples from the shipment | Sampling record |
| 3. Compare visually | Use the same lighting and approved reference | Visual inspection result |
| 4. Measure when needed | Use the agreed instrument and method | Color measurement report |
| 5. Make a decision | Accept, hold, or reject according to the agreed criteria | Inspection decision |
| 6. Report a mismatch | Share evidence with the manufacturer | Complaint and corrective action record |
I also consider the inspection method itself. The NIST publication CIE Fundamentals for Color Measurements discusses color measurement systems, viewing conditions, instruments, and measurement uncertainty. This reminds me that a measurement result needs suitable conditions and reliable equipment.
I do not assume that one visual check can prove every roll is identical. I use a consistent sampling plan and increase inspection when I find repeated problems. This helps me make a clear decision before the products reach my customers.
How Can Distributors Work With Manufacturers to Maintain Long-Term Color Consistency?
I cannot maintain repeat-order color consistency through inspection alone. I need my manufacturer to follow the same color standard, keep useful records, and communicate with me when a change may affect the product.
I build a stable process with shared references, batch records, regular quality reviews, and clear rules for approving changes. I also give the manufacturer accurate order information so that both sides can work toward the same result.

How Can I Build a Repeatable Color Management Process?
I ask the manufacturer to keep an approved color reference and link it to the correct product code. I also want the supplier to record the production batch and relevant color inspection results for important products.
When I place a repeat order, I use the same product code and reference sample. If the manufacturer needs to change a raw material, color formulation, surface finish, or production method, I ask for notification before the change affects my order.
I also agree on how the manufacturer should handle a color mismatch. The process should identify who investigates the problem, what evidence is required, and how both sides decide whether the batch meets the standard.
How Can I Review Performance Over Time?
I do not judge long-term performance from one successful shipment. I review the results across repeat orders and look for recurring differences.
For example, I can record the number of batches inspected, the number that failed the agreed color criteria, the time needed to resolve each issue, and whether the same problem happened again. These are useful business indicators, but I need to calculate them from my own order records. I should not treat them as universal industry benchmarks.
| Management practice | My action | Expected benefit |
|---|---|---|
| Shared color references | Keep the same approved sample and code | Reduces interpretation differences |
| Batch traceability | Link each shipment to its production records | Makes investigations easier |
| Change control | Require notice and approval for important changes | Reduces unexpected color variation |
| Regular reviews | Discuss inspection results and complaints | Helps identify recurring problems |
| Corrective actions | Record the cause and follow-up results | Helps prevent the same issue from returning |
| Clear communication | Confirm specifications before each order | Reduces avoidable order errors |
I also recognize that some products may need more attention than others. A standard color with stable demand may need routine checks, while a custom color for a large furniture project may need more detailed approval and measurement.
I want a manufacturer that can explain how it controls color, not just one that promises consistent results. I review the evidence, discuss problems openly, and update the process when my customers’ requirements change.
Long-term color consistency depends on shared responsibility. I need to provide clear requirements and manage my references carefully. My manufacturer needs to follow the approved standard, keep reliable records, and act quickly when a batch does not meet the agreed criteria.
Conclusion
I maintain color consistency by using approved samples, written tolerances, repeatable inspections, and clear communication with manufacturers across every edge banding order.
Data Sources
- International Organization for Standardization (ISO) — ISO/CIE 11664-4:2019: Colorimetry, Part 4: CIE 1976 Lab Colour Space*
https://www.iso.org/standard/74166.html
Defines the CIE 1976 Lab* color space and methods for representing color differences. - International Organization for Standardization (ISO) — ISO/CIE 11664-6:2022: Colorimetry, Part 6: CIEDE2000 Colour-Difference Formula
https://www.iso.org/standard/82662.html
Specifies the CIEDE2000 method for calculating color differences from CIELAB coordinates. - International Commission on Illumination (CIE) — Colorimetry, Part 4: CIE 1976 Lab Colour Space*
https://www.cie.co.at/publications/colorimetry-part-4-cie-1976-lab-colour-space-1
Provides technical information about the CIELAB color space and its use in color measurement. - National Institute of Standards and Technology (NIST) — CIE Fundamentals for Color Measurements
https://www.nist.gov/publications/cie-fundamentals-color-measurements-0
Discusses color measurement systems, instruments, viewing conditions, and measurement uncertainty.