A small edge banding defect may look harmless on one panel, but repeated across thousands of furniture parts, it can increase rework, waste materials, delay delivery, and damage customer trust.
I believe buyers can prevent most avoidable edge banding defects by checking three things: material consistency, processing conditions, and quality control. Buyers should approve samples, confirm machine compatibility, and set clear inspection standards before mass production begins.
When I look at edge banding quality, I do not focus only on the finished appearance. I also look at the production process behind it. A defect may come from the edge banding material, the adhesive, the panel, the machine, or the way the factory controls production. Buyers need to understand these factors because the same defect can have different causes. In the following sections, I will explain the common problems, show how buyers can identify their causes, and share practical steps to reduce defects in large orders.
What Are the Most Common Edge Banding Defects in Mass Production?
When furniture factories produce thousands of panels, even a small quality problem can affect many finished products. I recommend that buyers learn to identify common edge banding defects before they discuss solutions with suppliers.
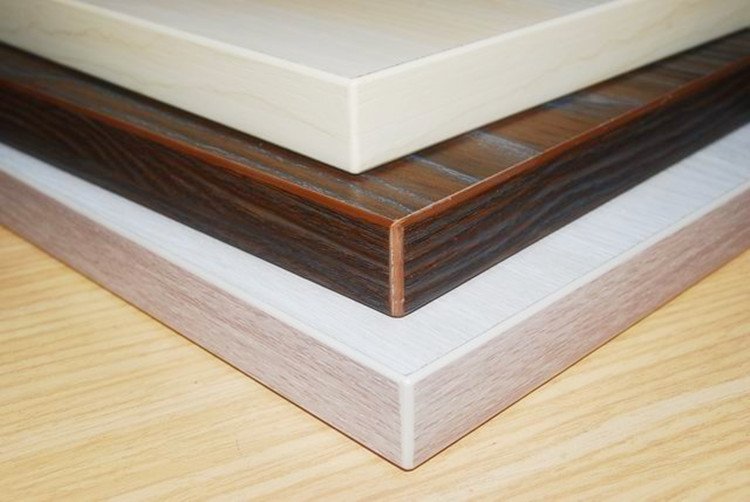
Edge banding defects usually appear as poor adhesion, visible gaps, uneven trimming, surface damage, color differences, or inconsistent dimensions. Buyers should record each defect and check whether it comes from the material, the processing equipment, or the production method.
Which Defects Should Buyers Check First?
In my experience, buyers should start with defects that affect product strength and appearance. These problems can lead to customer complaints and extra work on the production line.
1. Edge banding peeling or poor adhesion
The edge banding may separate from the panel during production or after the furniture is assembled. Buyers may see open gaps or find that the tape can be pulled away easily. Possible causes include incorrect adhesive settings, cold materials, poor surface preparation, or an unsuitable adhesive and material combination. SURTECO and REHAU both identify processing temperature, pressure, feed speed, and material conditions as important factors in bonding quality.
2. Open glue lines and visible gaps
A visible glue line can make a finished panel look less professional. The problem may come from an uneven panel edge, insufficient pressure, incorrect adhesive application, or unsuitable machine settings. Buyers should check whether the gap appears across the whole edge or only in certain areas.
3. Uneven trimming and rough corners
Excess material may remain along the panel edge, or the trimming process may leave rough corners and visible cutting marks. These problems can be related to cutter condition, cutting speed, machine alignment, and the selected edge banding thickness.
4. Scratches, dents, and surface marks
Surface damage may happen during manufacturing, transportation, storage, or processing. Buyers should inspect the material before production and then check finished panels. This helps them separate incoming material defects from damage caused by factory operations.
5. Color and dimension inconsistencies
Two rolls may look slightly different even when they use the same color reference. Width and thickness variations can also affect trimming and the final appearance. Some manufacturers note that slight color differences can occur between production batches, so buyers should confirm acceptable tolerances before ordering.
How Can Buyers Record These Defects?
I recommend using a simple defect classification system. It gives the supplier and furniture factory a shared way to discuss problems.
| Defect category | What buyers should check | Possible production impact |
|---|---|---|
| Adhesion | Peeling, open glue lines, weak bonding | Rework or panel rejection |
| Appearance | Scratches, dents, color variation | Inconsistent finished furniture |
| Dimensions | Width, thickness, length consistency | Poor trimming or fitting |
| Machining | Rough edges, chipped corners, cutting marks | Slower finishing and more rework |
| Handling | Damaged rolls, dirty surfaces, deformation | Material waste and production delays |
I would not treat every visible defect as proof of poor material quality. A good investigation should compare the incoming roll, the machine settings, and the finished panel. This approach helps buyers identify the real cause instead of asking the supplier to replace material that may not be defective.
What Causes Edge Banding Defects During Large-Scale Furniture Production?
A defect that appears during mass production does not always mean the edge banding itself is poor. In many cases, the problem comes from a mismatch between the material and the production conditions.
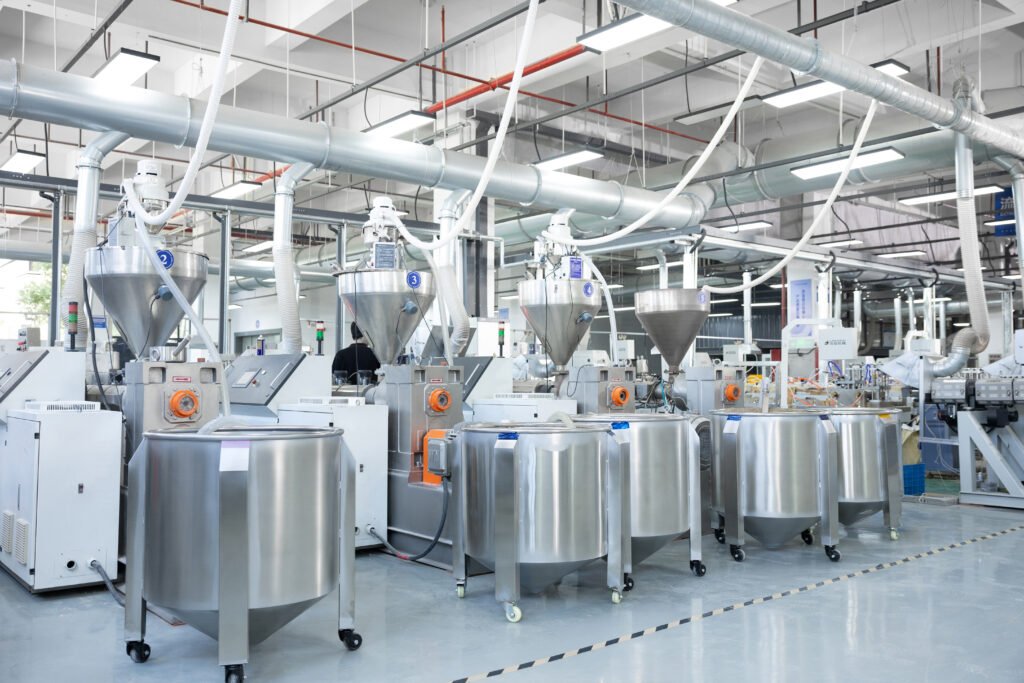
I recommend checking adhesive temperature, feed speed, pressure, panel condition, and machine setup first. These factors can affect bonding and trimming, especially when a factory changes materials or increases production speed.
How Do Machine Settings Affect Edge Banding Quality?
Hot-melt adhesive needs suitable processing conditions to bond the edge banding to the panel. If the adhesive cools too early, the bond may be weak. If the factory applies too little adhesive or too little pressure, the tape may not make full contact with the panel edge.
The REHAU troubleshooting guide identifies low room temperature, cold materials, low adhesive temperature, slow feed speed, and insufficient roller pressure as possible causes of poor adhesion. SURTECO also advises factories to check material temperature and processing conditions.
I would therefore avoid using one fixed machine setting for every edge banding product. Different materials, thicknesses, adhesives, and machines may need different settings. Buyers should ask their suppliers for product-specific processing guidance and confirm it through production trials.
Why Do Panel and Storage Conditions Matter?
The panel edge is the surface that receives the adhesive. If that surface is uneven, dusty, damaged, or too cold, the bonding result may change. The panel’s condition matters just as much as the edge banding’s condition.
Storage can also affect production. Some PVC edge banding technical data sheets recommend room-temperature storage and protection from direct sunlight or extreme temperatures. SURTECO recommends that both the panel and edge banding should be at room temperature, with 18°C as a minimum guideline for its processing instructions.
I would treat these values as product-specific guidance, not universal rules for every material. Buyers should follow the actual edge banding and adhesive manufacturers’ instructions.
Which Production Factors Should Buyers Investigate?
| Production factor | Possible effect | What I recommend checking |
|---|---|---|
| Adhesive temperature | Weak or inconsistent bonding | Actual application temperature and adhesive specifications |
| Feed speed | Adhesive may cool too early or machining quality may change | Machine speed and adhesive working range |
| Roller pressure | Incomplete contact with the panel | Pressure settings and roller condition |
| Panel edge condition | Gaps or uneven glue lines | Edge quality, cleanliness, and flatness |
| Material temperature | Faster adhesive cooling or processing issues | Storage and conditioning before use |
| Cutting tools | Rough trimming or chipped edges | Cutter condition, alignment, and speed |
I also recommend checking when the defect first appears. If it starts immediately after a material change, the new material may not match the existing settings. If it develops after several hours, buyers should investigate temperature stability, adhesive condition, tool wear, and other changes during the production run.
The key is to change one factor at a time and record the result. This gives the factory a clearer way to find the cause and avoid repeating the same problem on future orders.
How Do Edge Banding Materials and Supplier Quality Affect Production Defects?
I do not believe buyers should judge edge banding quality by appearance alone. A roll may look smooth and have the right color, but it can still cause problems when the factory processes it at high speed.
Material consistency, primer quality, dimensional accuracy, and batch control all matter. I recommend that buyers evaluate both the edge banding product and the supplier’s ability to keep quality stable across repeat orders.

Why Does Material Consistency Matter?
Different edge banding materials have different processing characteristics. PVC, ABS, acrylic, and other materials should not be treated as interchangeable products. Even within one material category, thickness, surface finish, formulation, and backing treatment can affect processing results.
For example, the primer on the back of edge banding helps the adhesive bond to the tape. If the primer is missing, damaged, or unsuitable for the selected adhesive, bonding may become unreliable. Buyers should ask suppliers to confirm the intended adhesive compatibility instead of assuming that every roll will work with every machine.
Dimensional consistency also matters. If the width or thickness changes between rolls, the factory may need to adjust its trimming or machining settings. These changes can increase setup time and make finished panels less consistent.
Color control is another important issue. A supplier may use the same color reference for two orders, but small differences between production batches can still occur. I recommend confirming color approval with physical samples and keeping a reference sample for future comparisons.
How Can Buyers Evaluate Supplier Quality?
I suggest asking suppliers for clear product specifications and records that relate to the actual order. A general statement such as “high quality” does not tell buyers how the product will perform in production.
| Supplier quality factor | What buyers should request | Why it matters |
|---|---|---|
| Material specifications | Material type, thickness, width, and tolerances | Helps confirm machine compatibility |
| Surface quality | Agreed standards for scratches, dents, and finish | Reduces appearance-related disputes |
| Backside treatment | Primer or bonding compatibility information | Supports reliable adhesion |
| Color consistency | Approved color sample and batch identification | Helps manage repeat orders |
| Production records | Batch number and inspection results | Makes quality problems easier to trace |
| Technical support | Processing instructions and troubleshooting guidance | Helps factories resolve production issues |
Should Buyers Choose the Cheapest Edge Banding?
I would compare the total cost of using a product rather than its purchase price alone. A lower-priced roll may still cost more if it causes frequent machine adjustments, material waste, or extra inspection.
For example, imagine a factory processes 10,000 panels in one production run. If 2% of the panels require rework, that means 200 panels need additional attention. This is a hypothetical example, not an industry defect-rate benchmark. The actual cost depends on the type of defect, labor, material waste, and whether the panels can be repaired.
This is why I recommend testing the product under real production conditions before placing a large order. Buyers should also review the supplier’s consistency across multiple batches, not just the quality of one approved sample.
A supplier who provides clear specifications, stable production quality, and useful technical support can help buyers reduce uncertainty. The goal is not simply to buy edge banding that looks good when it arrives. The goal is to buy material that works reliably in the intended production process.
How Can Buyers Prevent Edge Banding Defects Before Mass Production Begins?
I believe the best time to prevent defects is before the factory starts a large production run. Once thousands of panels have been processed, even a small mistake can become expensive to correct.
Buyers can reduce this risk by approving samples, confirming specifications, testing material compatibility, and setting clear acceptance criteria. These steps help both the buyer and supplier understand what the order must deliver.
Step 1: Confirm the Product Specifications
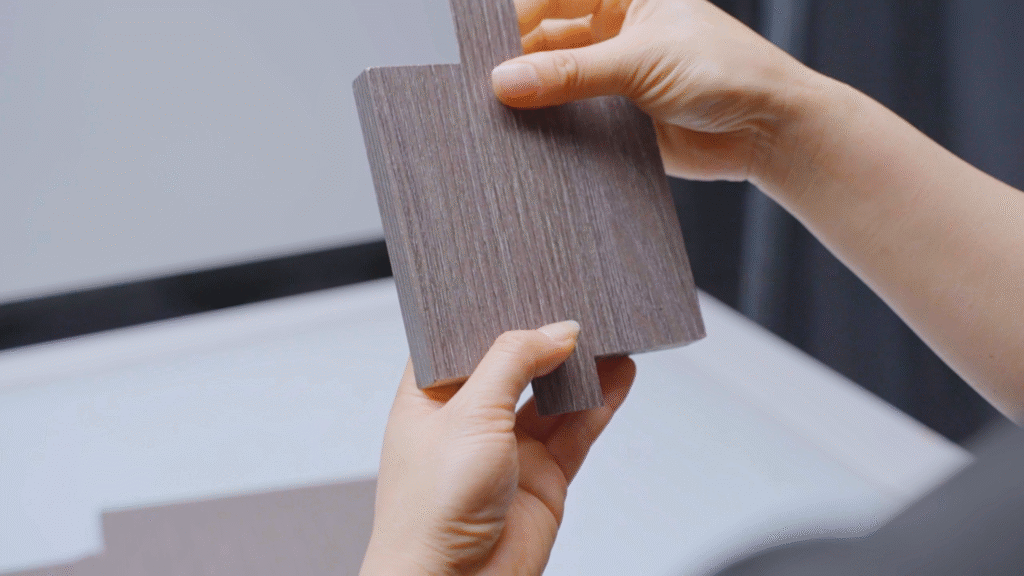
Before placing an order, I recommend confirming the material, color, surface finish, width, thickness, roll length, and packaging requirements. Buyers should also specify the panel type and intended application.
A product specification sheet can help prevent misunderstandings. For example, the phrase “white PVC edge banding” does not fully define the required product. The buyer may need a particular shade of white, a matte finish, a specific thickness, and a defined width tolerance.
I would also ask the supplier to identify the approved product version. If a later order uses a different formulation, finish, or backing treatment, the buyer should review whether the change affects production.
Step 2: Approve a Sample and Run a Production Trial
A sample approval is useful, but I would not rely on a small hand-applied sample alone. The factory should test the edge banding on the actual panel material and, where possible, on the machine that will handle mass production.
The trial should check bonding, trimming, corner quality, surface appearance, and color matching. The factory should also record the adhesive type, application temperature, feed speed, and other relevant settings.
SURTECO’s processing guidance recommends trials to determine suitable settings for the intended application. This supports an important purchasing principle: a material should be evaluated under the conditions in which it will actually be used.
Step 3: Agree on Acceptance Criteria Before Production
Buyers and suppliers should agree on what counts as acceptable and unacceptable quality. They should not wait until the goods arrive to decide whether a scratch, color difference, or dimensional variation is serious.
| Item to confirm | Recommended agreement |
|---|---|
| Appearance | Acceptable limits for scratches, dents, and surface marks |
| Color | Approved sample and method of comparison |
| Dimensions | Specified width and thickness tolerances |
| Bonding | Defined adhesion test and acceptance method |
| Packaging | Protection against contamination and damage |
| Traceability | Batch numbers and inspection records |
| Nonconforming goods | Reporting, investigation, and corrective-action process |
Step 4: Check Storage and Handling Requirements
Even a conforming product can develop problems if the factory stores it incorrectly. Buyers should share the supplier’s storage instructions with the production team and avoid leaving sensitive materials in unsuitable conditions.
I would also ask the factory to inspect the rolls before use. Workers should check the packaging, labels, visible surface condition, and product dimensions. The team should report damaged or questionable rolls before feeding them into the machine.
Step 5: Keep a Written Record of the Approved Process
A successful trial should create a repeatable process. I recommend recording the approved material, adhesive, machine settings, panel type, and inspection results. When the next order arrives, the factory can compare it with the original record instead of starting from zero.
This step is especially useful for buyers who purchase the same edge banding regularly. A written standard makes it easier to identify changes between batches and discuss them with the supplier. It also helps new production staff follow the same requirements.
In my view, pre-production approval should be treated as part of purchasing, not as an extra task. It gives buyers a chance to identify compatibility problems while the order is still manageable and before a defect affects the whole production line.
What Quality Control Measures Can Buyers Use to Reduce Defects in Repeat Orders?
I do not think one successful order proves that a supplier will deliver the same quality every time. Buyers need a repeatable inspection process that checks incoming materials, production performance, and finished products.
I recommend combining incoming inspection, in-process checks, batch traceability, and final inspection. A consistent quality control process helps buyers identify problems earlier and gives suppliers clear evidence when corrective action is needed.
How Should Buyers Inspect Incoming Materials?
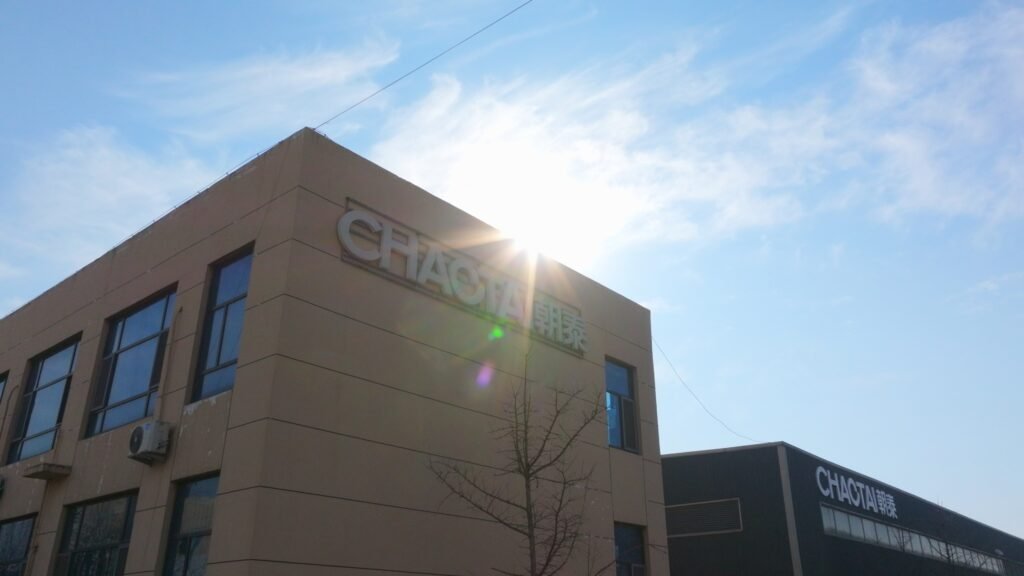
I recommend checking each incoming batch against the approved specifications before releasing it for production. The inspection should cover product labels, batch numbers, dimensions, color, surface condition, and packaging.
Buyers should also compare the material with the approved reference sample. If the new batch looks different, the quality team should record the difference and decide whether further testing is needed.
For dimensional checks, buyers should use suitable measuring tools and record actual results. They should not rely only on a supplier’s general statement that the material meets specifications.
How Can Buyers Monitor Quality During Production?
Incoming inspection cannot identify every problem. Some defects only appear when the material runs through the production line. For this reason, I recommend checking the first panels after machine setup and repeating inspections at planned intervals.
The factory should inspect bonding, glue lines, trimming, corners, and surface appearance. The team should also monitor whether defect frequency increases during the run.
I would pay special attention to the following situations:
- When a new roll or material batch enters production.
- When workers change adhesive or machine settings.
- When the production line restarts after a long stop.
- When the machine speed changes.
- When workers replace cutting tools or perform maintenance.
These checks help the factory detect changes before they affect a large number of panels. If a serious defect appears, the team should isolate potentially affected products and investigate the cause before continuing production.
How Can Buyers Use Sampling Standards?
For large orders, checking every item may not always be practical. Buyers can establish a sampling plan based on order size, defect severity, supplier performance, and the cost of failure.
The international standard ISO 2859-1:2026 provides sampling schemes for lot-by-lot inspection using Acceptance Quality Limit (AQL) criteria. Buyers can use an agreed sampling plan to define sample sizes and acceptance or rejection rules.
However, I would not treat AQL as a promise that a batch contains a specific percentage of defects. It is part of a statistical acceptance-sampling system. Buyers and suppliers need to agree on the inspection level, defect classifications, and acceptance criteria before applying it.
What Should a Repeat-Order Quality Control Plan Include?
| Control measure | When to use it | Main purpose |
|---|---|---|
| Incoming inspection | Before production | Confirm material compliance |
| First-piece inspection | After setup or material changes | Verify the production process |
| In-process sampling | At agreed production intervals | Detect changes during the run |
| Final inspection | Before shipment or release | Confirm finished-product requirements |
| Batch traceability | Throughout production | Identify affected materials and orders |
| Corrective-action records | When defects occur | Prevent the same problem from returning |
How Should Buyers Handle Repeated Defects?
When a defect occurs, I recommend recording the product batch, machine settings, panel type, adhesive information, and defect location. Photos and sample panels can help the buyer and supplier compare their findings.
The next step is to identify the cause and agree on corrective action. Replacing defective rolls may solve an immediate problem, but it does not necessarily prevent the same issue from happening again.
For example, if peeling occurs only when the production line runs at a particular speed, both parties should review the adhesive’s working range, material temperature, and machine settings. If color differences occur between batches, they should review color approval and batch control.
I also recommend tracking defects over several orders. If the same problem appears repeatedly, the buyer should request a documented investigation rather than treating each case as an isolated event.
In my view, repeat-order quality depends on more than the supplier’s final inspection. It requires shared standards, clear records, and a process for learning from previous problems.
Conclusion
I recommend that buyers prevent edge banding defects through pre-production trials, clear specifications, suitable processing conditions, and consistent quality control across every order.
Quality Control Process
Incoming material checks, in-line inspection and batch testing — how defects are kept out.
See our QC process
Data Sources and References
The following technical documents support the processing recommendations and quality control practices discussed in this article.
1. REHAU — Edgeband Processing: Troubleshooting and Processing Faults
https://www.rehau.com/downloads/500572/edgebandmaterialandprocessingtips-100711-rehau.pdf
Covers common adhesion and machining problems, including temperature, pressure, and feed speed.
2. SURTECO North America — Edgeband Troubleshooting
https://surteconorthamerica.com/edgebandtroubleshooting/
Explains possible causes of poor adhesion, open glue lines, and other edge banding processing problems.
3. SURTECO North America — Edgeband Processing
https://surteconorthamerica.com/edgebandprocessing/
Provides guidance on adhesive compatibility, processing temperatures, and material conditioning.
4. ISO — ISO 2859-1:2026, Sampling Procedures for Inspection by Attributes
https://www.iso.org/standard/2859-1
Defines acceptance-sampling schemes for lot-by-lot inspection using AQL criteria.
5. EGGER — Technical Datasheet: PVC Edging
https://www.egger.com/get_download/9df01599-836e-47bb-b3ae-e908d89e1913/Technical_datasheet_EGGER_Edging_PVC.pdf
Provides product-specific information on PVC edge banding and storage conditions.