When edge banding products fail to meet customer expectations, I lose more than a sale. I may face returns, extra shipping costs, production delays, and damaged business relationships.
I reduce product returns and customer complaints by setting clear specifications, checking product quality, testing samples, and working with reliable manufacturers. I also track complaints and use the results to prevent the same problems from happening again.
In my experience, I should not treat every complaint as an isolated problem. A complaint may point to a product defect, an unclear specification, poor storage, or a problem during furniture production. I need to find the real cause before I decide what action to take. This approach helps me protect my customers and build a more stable business.
Why Do Edge Banding Distributors Face Product Returns and Customer Complaints?
I know that even a small quality problem can create a large problem for a furniture manufacturer. A color mismatch or bonding failure may affect finished furniture, delay an order, and lead to a complaint against the distributor.
I usually look at product quality, order accuracy, storage conditions, and communication when I investigate returns. I also check whether the product meets the customer’s actual requirements.
What Are the Main Causes of Returns?
I first check whether the product matches the approved sample and written specifications. If the thickness, width, color, or surface finish is different, the customer may not be able to use the material as planned.
I also consider problems that happen after the products leave the factory. Poor storage, damaged packaging, incorrect handling, and unsuitable processing conditions can affect the final result. I should not automatically blame the manufacturer for every complaint, but I should not ignore manufacturing defects either.
How Can I Find the Real Cause of a Complaint?
I collect information before deciding who is responsible. I ask the customer for photos, batch numbers, order details, and a description of the problem. When possible, I also request a sample of the defective material and check how the customer processed it.
| Possible cause | What I check | Possible action |
|---|---|---|
| Color mismatch | Approved sample, color reference, and production batch | Confirm color standards and improve batch checks |
| Incorrect dimensions | Product measurements and order specifications | Check production settings and inspection records |
| Bonding failure | Adhesive, temperature, pressure, and processing speed | Test the complete bonding process |
| Surface defects | Product samples and production records | Improve process control and defect inspection |
| Damaged packaging | Shipping records and package condition | Improve packing and handling |
| Wrong product supplied | Purchase order, labels, and delivery documents | Strengthen order confirmation and labeling |
I also record how often each problem happens. If several customers report similar defects, I investigate whether the complaints share a common cause. I do not rely only on memory or informal messages.
The ISO 9001 quality management standard provides a framework for monitoring performance, meeting customer requirements, and improving processes. I can apply the same basic idea to my own complaint records. I use real evidence to identify recurring problems and decide where corrective action is needed.
Which Edge Banding Quality Problems Cause the Most Customer Complaints?
I pay close attention to the quality problems that can prevent customers from using edge banding as intended. A product may look acceptable when it arrives, but it may still cause trouble during processing or after the furniture is assembled.
I check dimensions, color, surface appearance, and bonding performance. I also make sure that the product suits the customer’s materials, equipment, and processing conditions.
How Do Color and Dimension Problems Affect Customers?
Color matching is important for furniture manufacturers that use decorative panels. If the edge banding does not match the panel, the finished product may look inconsistent. This can be a serious issue for cabinet doors, office furniture, and custom furniture projects.
I therefore ask customers to confirm the color reference and, when possible, compare the edge banding with the actual panel. I do not assume that two products will match simply because their color names are similar.
I also check thickness and width against the agreed specifications. Incorrect dimensions may affect trimming, edge coverage, or the finished appearance. I make sure that the customer and manufacturer use the same measurement standards before production starts.
Why Should I Check Surface Quality and Bonding Performance?
I look for scratches, dirt, uneven finishes, visible marks, and other defects that may affect the final product. These problems can come from production, packaging, transportation, or storage.
Bonding problems need a more careful review. Poor adhesion may be related to the edge banding, the adhesive, the machine settings, or the condition of the panel. For example, a bonding failure does not always mean that the edge banding itself is defective. I need to check the full process before deciding what went wrong.
| Quality issue | Possible effect | What I should verify |
|---|---|---|
| Color difference | Visible mismatch with furniture panels | Approved color sample and batch reference |
| Thickness or width deviation | Processing difficulties or poor edge coverage | Measurements against agreed tolerances |
| Surface defects | Poor finished appearance | Visual inspection and packaging condition |
| Poor adhesion | Edge lifting or bonding failure | Material compatibility and machine settings |
| Excessive brittleness or cracking | Damage during handling or processing | Material properties and processing conditions |
| Inconsistent finish | Different appearance between products | Surface specifications and production controls |
I also avoid using vague requirements such as “good quality” as the only acceptance standard. I define measurable specifications and agree on acceptable limits before placing an order.
For repeated orders, I keep approved samples and product records. These records give me a reference when I receive new stock or investigate a complaint. They also help me explain the problem to the manufacturer without relying on subjective descriptions alone.
How Can Distributors Prevent Quality Issues Before Products Reach Customers?
I believe prevention is more effective than dealing with every problem after delivery. Returns can involve transportation, inspection, replacement, and customer service. I can reduce these risks when I check product requirements before ordering and inspect the products before distribution.
I use clear specifications, sample approval, incoming inspection, and batch records to identify problems early. I also match the inspection process to the product risks and the supplier’s past performance.
How Can I Set Up a Practical Inspection Process?
I start by confirming the product details with the customer and manufacturer. These details may include material, color, thickness, width, finish, quantity, packaging, and intended application.
I then request a sample for approval. If the product will be used on a specific furniture panel or production line, I ask the customer to test it under normal processing conditions. A visual sample check alone may not reveal every problem.
When the order arrives, I check the packaging, labels, quantities, and product dimensions. I also inspect appearance and compare the products with the approved sample. For larger shipments, I can use a documented sampling plan instead of relying on a few items selected without a clear method.
The NIST Engineering Statistics Handbook explains acceptance sampling as a way to make lot acceptance decisions using randomly selected samples. Sampling can reduce inspection effort, but it does not guarantee that every item in a lot is defect-free. I still need a suitable inspection plan based on the product and the risks.
How Can I Manage Incoming Products More Consistently?
I use the same basic checklist for every relevant shipment. This helps me avoid missing important details when orders arrive during busy periods.
| Inspection stage | Action | Record to keep |
|---|---|---|
| Before ordering | Confirm specifications and sample approval | Approved sample and purchase order |
| During order confirmation | Verify quantity, color, dimensions, and packaging | Written order confirmation |
| At goods receipt | Check labels, quantity, and visible damage | Receiving inspection record |
| During product inspection | Measure samples and check appearance | Inspection results and photos |
| Before distribution | Confirm that the shipment meets agreed requirements | Release or hold decision |
I also separate products that show possible defects until I finish the investigation. I do not mix questionable stock with accepted inventory because this can make it harder to trace the problem later.
I keep records of supplier, batch, purchase order, inspection date, and complaint history. If I notice repeated problems, I increase attention to the affected product or supplier and ask for corrective action.
My inspection process does not need to be complicated. It needs to be consistent, documented, and based on clear requirements. These steps help me identify problems before they reach my customers and make it easier to explain any issue that still occurs.
What Should Distributors Expect From Their Manufacturer’s Quality Control Process?
I do not expect a manufacturer to promise that no defect will ever occur. I expect the manufacturer to have a clear process for preventing defects, finding problems, and responding when something goes wrong.
I look for documented specifications, production checks, final inspection, batch traceability, and a clear complaint-handling process. I also want the manufacturer to explain how it investigates repeated defects and prevents them from happening again.
What Quality Controls Should a Manufacturer Provide?
I first ask how the manufacturer confirms product requirements before production. The manufacturer should understand the agreed material, dimensions, color reference, surface finish, and packaging requirements.
I then ask how quality is checked during production. Depending on the product and process, the manufacturer may measure dimensions, inspect the surface, check color consistency, and monitor other important production conditions.
Final inspection is also important. I want to understand how the manufacturer checks the finished products before packing and shipping. I may ask for inspection records, product photos, or batch information when these are relevant to my order.
ISO 9001 provides a recognized framework for quality management, including process control, performance evaluation, customer focus, and continual improvement. However, I do not treat a certificate as proof that every product is defect-free. I still review the actual controls used for my products and check whether the manufacturer meets our agreed requirements.
How Should a Manufacturer Handle Complaints?
I expect the manufacturer to respond with facts rather than simply deny responsibility. A good investigation should identify the affected batch, review production records, examine samples when available, and consider possible causes during transport and customer processing.
I also expect a clear plan for the next steps. Depending on the findings and the agreement between both parties, this may include replacement products, a credit, a revised inspection process, or other corrective action.
| Manufacturer practice | What I ask for | Business value |
|---|---|---|
| Specification control | Written and confirmed product requirements | Reduces misunderstandings |
| Process inspection | Checks at relevant production stages | Helps detect defects earlier |
| Final inspection | Defined release criteria | Reduces the risk of shipping nonconforming products |
| Batch traceability | Batch identifiers and production records | Supports faster investigations |
| Complaint management | A clear contact and response process | Improves problem resolution |
| Corrective action | Cause analysis and prevention steps | Reduces repeated problems |
I also review how the manufacturer responds over time. One successful inspection does not prove that every future order will be consistent. I look at repeat-order quality, delivery performance, complaint handling, and the willingness to improve.
For me, the best manufacturer is not simply the one that claims to have strict quality control. It is the one that can explain its process, provide useful evidence, and work with me to solve problems when they occur.
How Can Better Quality Management Reduce Costs and Improve Distributor Profitability?
I know that product returns affect more than the value of the returned goods. I may also pay for shipping, inspection, storage, replacement orders, and customer support. I can protect my margins when I prevent avoidable defects and reduce the time spent solving repeated problems.
I measure quality management by its effect on real business results. I track return costs, complaint frequency, replacement orders, and the time needed to resolve each issue instead of assuming that better inspection will automatically increase profits.
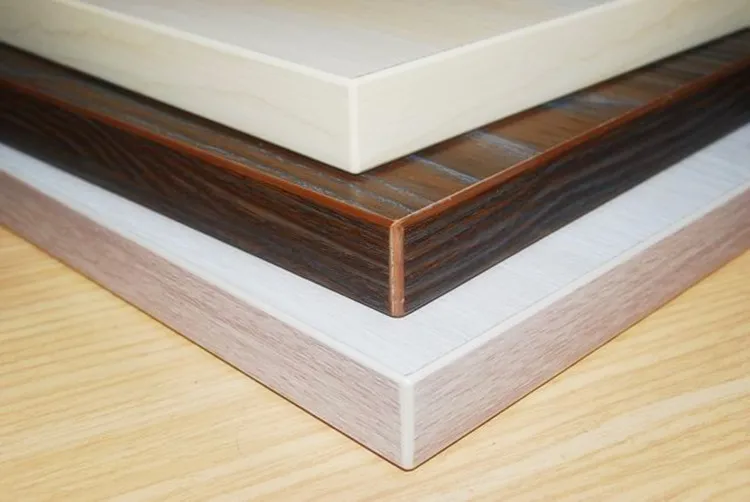
How Can I Calculate the Cost of Product Returns?
I begin by recording the direct and indirect costs of each complaint. Direct costs may include the value of defective goods, return freight, and replacement shipping. Indirect costs may include staff time, extra warehouse work, delayed customer orders, and lost repeat business.
For example, I may compare two suppliers with different purchase prices. One supplier may offer a lower price but generate more complaints. The other may charge more but provide products that meet my requirements more consistently. I need to compare the full cost of each option before deciding which supplier offers better value.
I can use a simple calculation:
Total quality-related cost = defective product cost + return and replacement costs + inspection and handling costs + other documented costs.
I should avoid counting the same expense twice. I should also separate confirmed costs from estimated losses, such as possible future sales that I cannot prove I have lost.
Which Indicators Should I Track?
I choose a small set of indicators that I can measure consistently. I use the same reporting period and clear definitions so I can compare suppliers and identify changes over time.
| Indicator | How I measure it | What it tells me |
|---|---|---|
| Return rate | Returned units divided by units delivered | How often products are returned |
| Complaint rate | Orders with complaints divided by total orders | How frequently customers report problems |
| Cost of returns | Documented costs linked to returns | The financial impact of quality issues |
| Repeat defect rate | Recurring defects divided by recorded defects | Whether corrective actions are working |
| Resolution time | Time from complaint to agreed resolution | How quickly problems are handled |
| Supplier acceptance rate | Accepted inspected lots divided by inspected lots | How often shipments meet the agreed acceptance rules |
I use these figures to identify trends rather than judge a supplier from a single month. I also check the order volume and product mix because a supplier with more orders may receive more complaints in absolute numbers without having a higher complaint rate.
The ISO 9001 quality management framework supports the use of performance evaluation and continual improvement. I can apply this principle by reviewing my records regularly and discussing the results with my manufacturers.
When I find a repeated problem, I agree on an action, set a review date, and check whether the data improves. If the same defect continues, I investigate again instead of treating each complaint as a separate event.
Better quality management does not remove every business risk. It gives me clearer information, reduces avoidable costs, and helps me make better purchasing decisions. Over time, this can support stronger customer relationships and more stable profitability.
Conclusion
I reduce returns by setting clear standards, inspecting products, tracking complaints, and working with manufacturers that can prove their quality controls and improve when problems occur.
Data Sources
- International Organization for Standardization (ISO) — ISO 9001: Quality Management Systems
https://www.iso.org/standard/9001
Supports the discussion of quality management, customer requirements, performance evaluation, and continual improvement. - National Institute of Standards and Technology (NIST) — Engineering Statistics Handbook: What Is Acceptance Sampling?
https://www.itl.nist.gov/div898/handbook/pmc/section2/pmc21.htm
Explains sampling-based inspection and how samples can support decisions about product lots. - International Organization for Standardization (ISO) — ISO 2859-1: Sampling Procedures for Inspection by Attributes
https://www.iso.org/standard/2859-1
Provides an international framework for acceptance sampling plans based on the Acceptance Quality Limit (AQL).